As a supplier of rotary lobe pumps, I am often asked whether these pumps can be used in hygienic applications. The answer is a resounding yes, and in this blog post, I will delve into the reasons why rotary lobe pumps are well - suited for hygienic environments, their design features that ensure hygiene, and some common applications in the hygienic sector.
Understanding Rotary Lobe Pumps
Rotary lobe pumps are positive - displacement pumps. They operate by two or more lobes rotating within the pump housing. As the lobes rotate, they create chambers that expand to draw fluid into the pump and then contract to push the fluid out. This mechanism allows for a smooth, gentle pumping action, which is ideal for handling sensitive fluids.
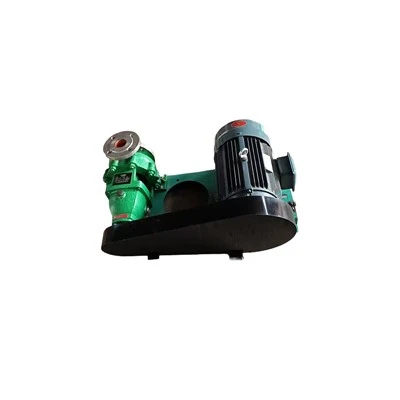
One of the key advantages of rotary lobe pumps is their ability to handle a wide range of viscosities. Whether it's a thin liquid like water or a thick substance like yogurt, rotary lobe pumps can transfer the fluid efficiently. For high - viscosity applications, our High Viscosity Lobe Pump is specifically designed to provide the necessary power and performance.
Design Features for Hygiene
Material Selection
In hygienic applications, the materials used in pump construction are of utmost importance. Our rotary lobe pumps are typically made from high - grade stainless steel. Stainless steel is corrosion - resistant, non - toxic, and easy to clean, which makes it an ideal choice for handling food, pharmaceuticals, and other sensitive products. Our Stainless Steel Lobe Pumps are crafted from top - quality stainless steel to ensure long - term durability and compliance with hygiene standards.
Easy to Clean
Cleanability is a critical factor in hygienic applications. Rotary lobe pumps are designed with smooth internal surfaces and minimal dead space. This design feature prevents the accumulation of product residues, which can harbor bacteria and cause contamination. Additionally, many of our pumps are designed for Clean - in - Place (CIP) and Sterilize - in - Place (SIP) processes. CIP allows the pump to be cleaned without disassembly, using a cleaning solution that circulates through the pump. SIP, on the other hand, takes the cleaning process a step further by sterilizing the pump to eliminate any remaining microorganisms.
Sealing Technology
Proper sealing is essential to prevent leakage and contamination. Our rotary lobe pumps are equipped with advanced sealing systems. These seals are designed to withstand the harsh chemicals used in cleaning and sterilization processes while maintaining a tight seal. This ensures that the pumped fluid remains contained within the pump and does not come into contact with the external environment, reducing the risk of contamination.
Hygienic Applications of Rotary Lobe Pumps
Food and Beverage Industry
The food and beverage industry requires strict adherence to hygiene standards. Rotary lobe pumps are widely used in this sector for handling a variety of products, including dairy products, fruit juices, sauces, and syrups. Their gentle pumping action ensures that the product's integrity is maintained, preventing damage to delicate ingredients such as fruit particles. For example, when pumping yogurt, the pump needs to transfer the product without disturbing its texture. Our Sanitary Rotary Lobe Pump is specifically engineered for such applications, meeting the highest hygiene standards in the food industry.


Pharmaceutical Industry
In the pharmaceutical industry, product purity is of the utmost importance. Rotary lobe pumps are used for transferring various pharmaceutical ingredients, including drugs, vaccines, and ointments. The pumps' ability to handle different viscosities and their cleanability make them a reliable choice for this industry. They can be easily sterilized to ensure that the pumped products are free from contaminants.
Cosmetics Industry
The cosmetics industry also benefits from the use of rotary lobe pumps. These pumps are used for handling creams, lotions, and other cosmetic products. The gentle pumping action prevents the shearing of the product, which can affect its consistency and quality. The hygienic design of the pumps ensures that the cosmetic products remain free from bacteria and other contaminants.
Advantages of Using Rotary Lobe Pumps in Hygienic Applications
Product Preservation
As mentioned earlier, the gentle pumping action of rotary lobe pumps helps preserve the integrity of the pumped product. This is particularly important in industries where the quality of the product is directly related to its texture, flavor, or chemical composition. For example, in the production of fine wines, the pump needs to transfer the wine without causing excessive agitation, which could affect the wine's taste and aroma.
Energy Efficiency
Rotary lobe pumps are generally energy - efficient. Their positive - displacement design allows them to pump fluid at a consistent rate, regardless of the pressure. This means that they do not waste energy by over - pumping or under - pumping. In large - scale hygienic applications, such as food processing plants, energy efficiency can lead to significant cost savings over time.
Versatility
Rotary lobe pumps are highly versatile. They can be used for a wide range of applications, from low - viscosity fluids to high - viscosity substances. This versatility makes them a valuable asset in industries where multiple products with different properties need to be pumped. For example, a food processing plant may use a single type of rotary lobe pump to handle both water - based sauces and thick pastes.
Our Product Range for Hygienic Applications
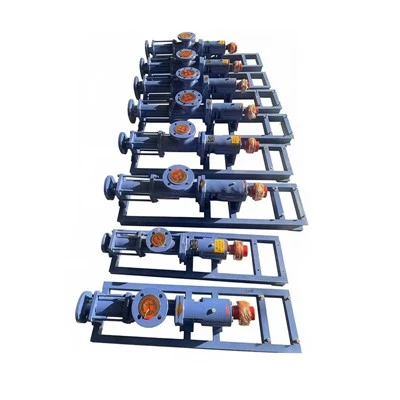
We offer a comprehensive range of rotary lobe pumps suitable for hygienic applications. Our Cam Rotor Pump is a popular choice for many customers. It combines reliability, efficiency, and hygiene in a single package. The cam rotor design provides a smooth and continuous flow, making it ideal for handling sensitive fluids.
Our Sanitary Rotary Lobe Pump is specifically designed to meet the strict hygiene requirements of the food, pharmaceutical, and cosmetics industries. It is made from high - grade stainless steel, has a smooth internal surface, and is compatible with CIP and SIP processes.
If you are dealing with high - viscosity products, our High Viscosity Lobe Pump is the perfect solution. It has a powerful motor and a robust design to handle thick fluids with ease.
And for those who need a durable and hygienic pump, our Stainless Steel Lobe Pumps are an excellent choice. The corrosion - resistant stainless steel construction ensures a long service life and compliance with hygiene standards.
Conclusion
In conclusion, rotary lobe pumps are well - suited for hygienic applications. Their design features, including material selection, cleanability, and sealing technology, make them a reliable choice for industries that require strict adherence to hygiene standards. Whether you are in the food and beverage, pharmaceutical, or cosmetics industry, our rotary lobe pumps can meet your needs.
If you are interested in learning more about our rotary lobe pumps for hygienic applications or would like to discuss your specific requirements, we encourage you to contact us to start a procurement discussion. We look forward to working with you to find the best pump solution for your business.
References
- "Positive Displacement Pumps: Principles and Applications" by John Smith
- "Hygienic Design in the Food Industry" by Sarah Johnson
- "Pump Selection Guide for the Pharmaceutical Industry" by Mark Davis