Can an aluminum diaphragm pump be used for food - grade applications?
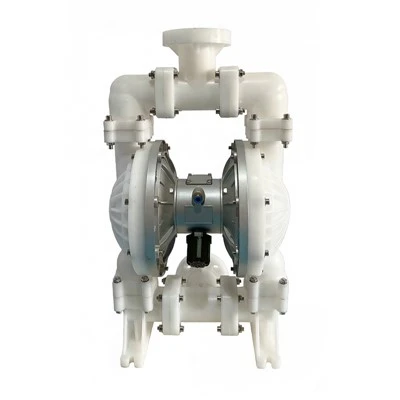
As a supplier of aluminum diaphragm pumps, I often receive inquiries from customers about whether our pumps can be used in food - grade applications. This is a crucial question, as the safety and quality of food products are of utmost importance. In this blog, I will explore the feasibility of using aluminum diaphragm pumps for food - grade applications, considering various factors such as material compatibility, design, and regulatory compliance.
Material Compatibility
Aluminum is a commonly used material in diaphragm pumps due to its lightweight, corrosion - resistant, and cost - effective properties. However, when it comes to food - grade applications, the compatibility of aluminum with food substances is a key concern.
Pure aluminum has a relatively high reactivity, and it can react with certain acidic or alkaline food products. This reaction may lead to the leaching of aluminum ions into the food, which can be harmful to human health. For example, aluminum can react with citric acid in fruits or vinegar in pickled products. To address this issue, many aluminum diaphragm pumps are coated or anodized. Anodizing is an electrochemical process that forms a protective oxide layer on the surface of the aluminum. This layer acts as a barrier, preventing direct contact between the aluminum and the food, and significantly reducing the risk of aluminum leaching.


In addition to the aluminum body, the diaphragm material is also critical. Diaphragms in food - grade pumps are typically made of materials such as EPDM (Ethylene Propylene Diene Monomer), PTFE (Polytetrafluoroethylene), or other food - grade elastomers. These materials are non - toxic, resistant to a wide range of food substances, and meet the relevant food safety standards.
Design Considerations
The design of an aluminum diaphragm pump for food - grade applications must ensure easy cleaning and sanitation. A well - designed pump should have smooth internal surfaces to prevent the accumulation of food particles and bacteria. Dead spaces, where food can get trapped, should be minimized.
The pump should also be designed for disassembly. This allows for thorough cleaning of all components, including the diaphragm, valves, and chambers. Regular cleaning is essential to maintain the hygiene of the pump and prevent the growth of harmful microorganisms. Some pumps are equipped with quick - release mechanisms, which make disassembly and reassembly much faster and more convenient.
Another important design aspect is the sealing. Proper sealing is necessary to prevent leakage of food products. Leakage not only leads to product loss but also increases the risk of contamination. High - quality seals made of food - grade materials should be used to ensure a tight and reliable seal.
Regulatory Compliance
Food - grade applications are subject to strict regulations and standards. In the United States, the Food and Drug Administration (FDA) has established guidelines for materials that come into contact with food. These guidelines specify the allowable materials, their composition, and the maximum allowable levels of migration of substances into food.
In the European Union, the European Food Safety Authority (EFSA) and the relevant national authorities enforce similar regulations. For example, materials used in food - contact applications must comply with the EU Regulation (EC) No 1935/2004.
As a supplier, we ensure that our aluminum diaphragm pumps meet these regulatory requirements. We source materials from reliable suppliers and conduct regular testing to verify the compliance of our pumps. Our pumps are also labeled with information about their food - grade suitability and the relevant regulatory certifications.
Advantages of Using Aluminum Diaphragm Pumps in Food - Grade Applications
Despite the challenges, there are several advantages to using aluminum diaphragm pumps in food - grade applications.
Firstly, aluminum diaphragm pumps are self - priming. This means that they can start pumping without the need for external priming, which is very convenient in food processing operations. They can handle a wide range of viscosities, from thin liquids like water to thick pastes like tomato sauce.
Secondly, these pumps are relatively simple in design and easy to operate. They require less maintenance compared to some other types of pumps, which can reduce downtime and operating costs in food production facilities.
Thirdly, aluminum diaphragm pumps can be powered by different sources, such as electricity or compressed air. This flexibility allows them to be used in various food processing environments. For example, in areas where electricity is not available or where explosion - proof requirements exist, air - powered pumps can be a suitable choice. You can explore our Explosion Proof Diaphragm Pump for such applications.
Limitations and Precautions
While aluminum diaphragm pumps can be used for food - grade applications, there are some limitations and precautions that need to be taken.
As mentioned earlier, the reactivity of aluminum with certain food substances is a concern. Therefore, it is important to carefully select the pump based on the specific food product to be pumped. For highly acidic or alkaline foods, pumps with more corrosion - resistant materials or coatings may be required.
Regular maintenance and inspection are also essential. The diaphragm, seals, and other components should be checked regularly for wear and tear. Any damaged parts should be replaced immediately to ensure the proper functioning and safety of the pump.
Conclusion
In conclusion, an aluminum diaphragm pump can be used for food - grade applications, provided that proper material selection, design, and regulatory compliance are ensured. The use of anodized aluminum and food - grade diaphragm materials, along with a well - designed pump structure, can minimize the risk of contamination and ensure the safety of food products.
Our company offers a wide range of aluminum diaphragm pumps suitable for food - grade applications. We also provide Small Electric Diaphragm Pump for small - scale food processing operations and Airless Diaphragm Pump for specific requirements.
If you are interested in our aluminum diaphragm pumps for food - grade applications, please feel free to contact us for more information and to discuss your specific needs. We are committed to providing high - quality products and excellent service to meet your food processing requirements.
References
- Food and Drug Administration (FDA). Guidelines for food - contact materials.
- European Food Safety Authority (EFSA). Regulations on food - contact materials in the EU.
- Manufacturer's specifications and technical documents for aluminum diaphragm pumps.